
Why do industrial systems require anti-freeze/coolant in the summer?
1405/03/02
Cooling Tower Chemical Cleaning Steps — Implementation Guide
1405/02/07
Types of sediments in RO systems and methods for identifying them
1405/02/05
Why is the use of general acids prohibited in boiler cleaning? (Danger of explosion and corrosion)
1404/12/06
Benefits of using specialized solutions from Abrizan Company for MED

Do you know why many industries are turning to Abrizan’s specialty solutions for MED systems after years of using generic materials?⚠️
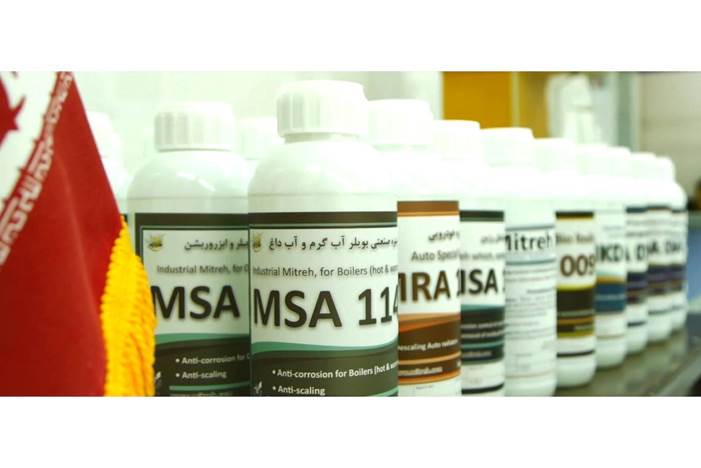
The use of specialty chemical solutions in multi-stage desalination (MED) systems not only prevents corrosion and scale, but also reduces operating costs by up to 25% and doubles the life of the equipment. Abrizan’s Mitreh brand products are designed with customized formulations, precisely based on the unique chemical challenges of each MED system.
Why are generic solutions not enough for MED systems?
MED systems operate in conditions of high temperatures, extreme salt concentrations and variable pH. Generic chemicals:
- Decompose at high temperatures
- React adversely with sulfate or silica ions
- Do not provide adequate corrosion protection for copper alloys or stainless steel
In contrast, specialty water treatment solutions are formulated with three key factors in mind—feedwater composition, equipment alloy type, and operating pattern.
⚙️ Four key advantages of Mitreh solutions in MED systems
➕ 1. Targeted prevention of complex scale types
MED systems typically encounter a combination of scales:
- Calcium carbonate (CaCO₃)
- Calcium sulfate (CaSO₄)
- Silica (SiO₂)
- Magnesium hydroxide (Mg(OH)₂)
Mitreh brand anti-scale and anti-scale products contain dispersant polymers and crystal inhibitors that:
- Inhibit the formation of scale nuclei
- Keep fine particles in suspension
- Effective even at high TDS concentrations (up to 70,000 ppm)
If you want to know what type of scale is dominant in your system, read the article [Scales and corrosion in MED desalination plants].
➕ 2. Intelligent multi-faceted corrosion protection
In MED, corrosion can occur from three main sources:
1. Oxygen corrosion (due to air leakage)
2. Acid corrosion (in low pH conditions)
3. Stress corrosion cracking (in sensitive alloys)
Mitreh thermal system anti-corrosion products:
- Contain film-forming inhibitors (such as molybdate and nitrite)
- Combined with liquid oxygen scavengers (such as substituted hydrazine or carbozide)
- Compatible with copper alloys, 316L stainless steel and titanium
✅ Technical note: In MED systems, the use of nitrite-free anti-corrosion agents is recommended to prevent the formation of nitrosamines (carcinogens) — and Mitreh offers such formulations.
➕ 3. Control biofouling without damaging equipment
Biofilms grow in the colder MED effects (usually effects 4 and above). Using chlorine or hypochlorite in these systems is dangerous because:
- It causes pitting corrosion in stainless steel
- It reacts with ammonium ions to produce toxic trihalomethanes
In contrast, non-oxidizing “mitreh” biocides (such as DBNPA and stabilized glutaraldehyde) and biodispersants:
- Remove biofilm from the surface
- Operate without increasing the risk of corrosion
- Stable at 40–60°C
➕ 4. Compatibility with chemical wash processes
Even the best antifouling program sometimes requires periodic washdown. Mitreh products are designed as an integrated ecosystem:
- Mild acid washes (citric or acetic based) for carbonate deposits
- Acid-based descalers for sulfate and silica
- Alkaline detergents for grease and biofilm
- Neutralizers and degreasers after washing
This coordination prevents side reactions between the different materials. For the correct implementation of this process, see the [MED Desalination Chemical Wash Steps] guide.
How do waterborne solutions increase ROI?
Many people think that specialty materials are “more expensive.” But in reality:
Cost | With general materials | With Mitreh solutions |
Chemical consumption per year | 100units | 70units |
Line stoppage due to sediment | 2times/year | 0.5times/year |
Replacing pipes | Every 3 years | Every 7 years |
Steam consumption | 100% | 85% |
Real data: A refinery in southern Iran reduced steam consumption by 12% and unplanned shutdowns by 70% after replacing generic materials with Mitreh thermal antifouling.
❓❓❓FAQs about using eluent solutions in MED❓❓❓
❓ Are these materials compatible with our RO or MSF systems alongside MED?
Yes. Mitreh formulations are also optimized for combined systems (such as MED + RO). For example, their antifoulings do not clog the RO membrane and do not cause problems in the desalination unit.
❓ Do we need to change the dosing system?
No. All Mitreh products are supplied as ready-to-use solutions or soluble powders and are compatible with standard dosing systems.
❓ How do we make sure that these materials are suitable for our system?
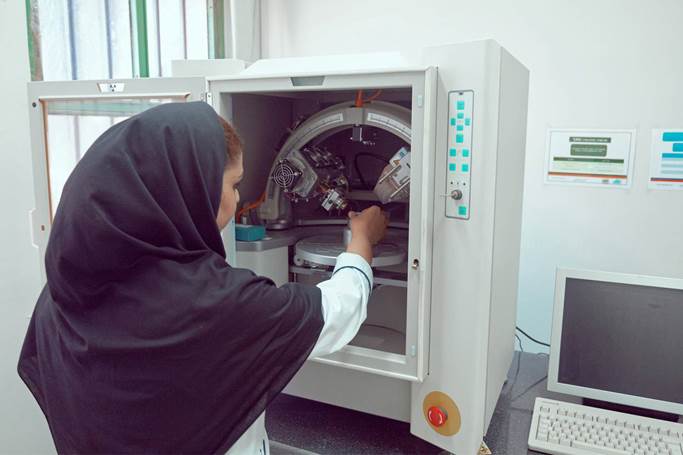
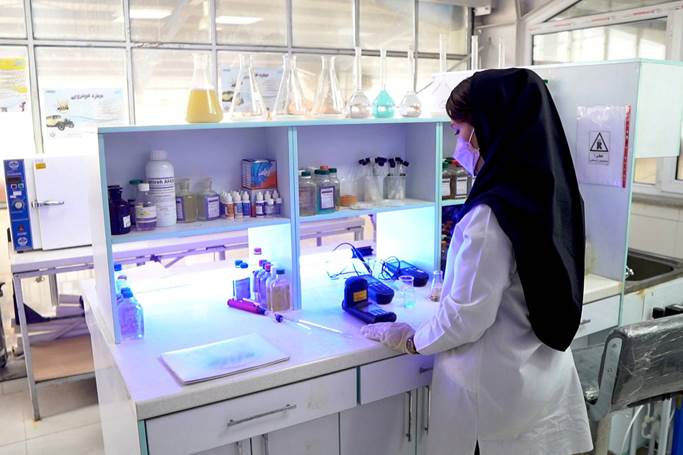
Abrizan Company offers free laboratory services and consultations:
- Feedwater analysis
- Sediment type identification
- Alloy compatibility testing
- Operational simulation in the laboratory
If you observe symptoms such as decreased production or increased temperature, first read the article [Signs of the need for chemical flushing of MED desalination plants].
❓ Why do large industries choose Abrizan?
- ✅ Domestic formulation: No dependence on imports
- ✅ 24/7 technical support: On-site engineering team
- ✅ ISO 17025 laboratory: Data-driven, not guesswork
- ✅ Experience in sensitive industries: oil, gas, power plants, petrochemicals
Also, Abrizan is the only manufacturer in Iran that offers specialized scale removers for hydrocarbon compounds and acid-base descalers with integrated corrosion inhibitors — features that are vital in oil units connected to MED.
✍️ Conclusion: Expertise is the Difference
In complex systems like MED, one size does not fit all. Mitreh’s specialist solutions are not only designed based on water chemistry, but also formulated with a deep understanding of the industry’s operational challenges. This combination allows industries to not only pay less but also significantly increase system reliability.
If you want to know what challenges your MED system faces, first review the article [Introduction to MED Systems and Their Chemical Challenges] — then explore the specialist solutions.
If you need expert advice… ⭐⭐⭐⭐⭐
If you need expert advice to identify the type of sediment or the optimal selection of chemicals, Abrizan’s specialists, with over 20 years of experience in advanced laboratories, are ready to provide customized solutions to various industries.
share :
Why do industrial systems require anti-freeze/coolant in the summer?
1405/03/02Cooling Tower Chemical Cleaning Steps — Implementation Guide
1405/02/07Types of sediments in RO systems and methods for identifying them
1405/02/05Why is the use of general acids prohibited in boiler cleaning? (Danger of explosion and corrosion)
1404/12/06
Related articles
Why is the use of general acids prohibited in boiler cleaning? (Danger of explosion and corrosion)
Using hydrochloric acid in boiler cleaning causes severe corrosion and explosion hazard. Experience safe descaling without damaging the metal with Mitreh Abrizan's specialized solution. Free consultation.
Chemical vs. Mechanical Washing in MED: Which Method is Better?
Which method is better for cleaning MED devices? Technical comparison, cost and risk of chemical vs. mechanical cleaning.
When is the best time to thermal desalination plant washing?
Signs of need for thermal desalination plant flushing (MED/MSF) + Data-based decision-making guide.

Common challenges in desalination plant maintenance and practical solutions
6 key challenges in power plant desalination plant maintenance + practical solutions to prevent power generation outages.
Types of deposits and corrosion in heat exchangers and identification methods
A comprehensive guide to identifying calcium carbonate, sulfate, silica, iron oxide, and MIC corrosion deposits in heat exchangers using XRD and SEM methods.
Step-by-step guide to chemical boiler cleaning — professional and safe execution
Step-by-step guide to chemical boiler cleaning in compliance with ASME standards, from system shutdown to final passivation. Safe and effective execution.
Warning signs that indicate the need for chemical cleaning of the heat exchanger
Has your heat exchanger lost its efficiency? 5 warning signs (increasing temperature, decreasing ΔT, high pressure, leakage, bad smell) + quick diagnosis checklist.
Comparison of boiler cleaning methods — chemical, mechanical or hydrojet
Which boiler cleaning method is best for you? A complete comparison of chemical, mechanical, and hydrojet methods in terms of cost, safety, time, and efficiency.
Submit your opinion
Your email address will not be published.